
Research article · 2023 · Full text
International Journal of Statistics and Applied MathematicsOptimize the Taguchi method, the signal-to-noise ratio, and the sensitivity
Volume 8(6) · Pages 64–70 · DOI: 10.22271/maths.2023.v8.i6a.1406 ↗
Research areasOptimal Experimental Design MethodsIndustrial Vision Systems and Defect DetectionAdvanced Statistical Process Monitoring
Abstract
Author-writtenStatistical quality control methods are a collection of strategies and scientific techniques to study many different complex production problems, which is an essential aspect of ensuring. The product is of a good enough quality to meet expectations. Quality control is a broad field with many subfields to research. One of the key parameters used in quality control is the signal-to-noise ratio (S/N). Which measures a product's quality by comparing the desired signal with the noise or unwanted variation output. The Taguchi method is an important statistical technique in quality control. Taguchi made contributions to the advancement and creation of sophisticated techniques in quality control models. The S/N ratio is an integral part of the Taguchi. That method is widely used in various manufacturing fields. The sensitivity analysis method is another important aspect of quality control that involves analyzing the impact of variations in the input factors on the output quality. Using the S/N ratio and sensitivity analysis, the Taguchi method can effectively improve product quality, reduce production costs, and minimize output variation. This makes the Taguchi method a good tool for quality control in various industries.
Summary
Source-checkedPlain-language reading of the full paper, prepared with AI and checked against the text. Each point links to the authors' own words.
Why it matters
- Statistical quality control uses scientific techniques to address complex production problems, ensuring products meet quality expectations. View evidence ↗
- The signal-to-noise (S/N) ratio is a critical quality control parameter that compares desired signals against unwanted variation (noise). View evidence ↗
- Sensitivity analysis is used in quality control to determine how variations in input factors affect the final output quality. View evidence ↗
The question
- The study aims to distinguish between significant and non-significant variables and determine the optimal S/N ratio, actual S/N ratio, gain, and variability reduction. View evidence ↗
What they did
- The research applied its methodology to data regarding Lime Saturation Factors (L.S.F) of cement. View evidence ↗
- Data was collected from chemical laborers with a sample size of 7*16. View evidence ↗
- The study used a Taguchi Orthogonal Array Design (L16(25)) consisting of 16 runs with 5 variables at two levels. View evidence ↗
What they found
- Variables X1, X2, and X4 at level 1 showed higher S/N ratios, suggesting a strong impact on variability. View evidence ↗
- Sensitivity analysis indicated that X4 and X5 at level 1 have a relatively strong impact on variability. View evidence ↗
- The calculated gain between the current and optimal condition was 0.009, resulting in a 0.101% reduction in variability. View evidence ↗
What it means
- The authors conclude that variables X1 through X5 exhibit higher S/N ratios, indicating they have a relatively strong impact on variability. View evidence ↗
Visual summary
2 visualsIllustrations explain the paper; charts are replotted from the paper's own table values.
Quality Control Framework
AI-generated conceptual illustration (industrial precision-machined steel gears). It explains the idea and does not show study data.
View source evidence ↗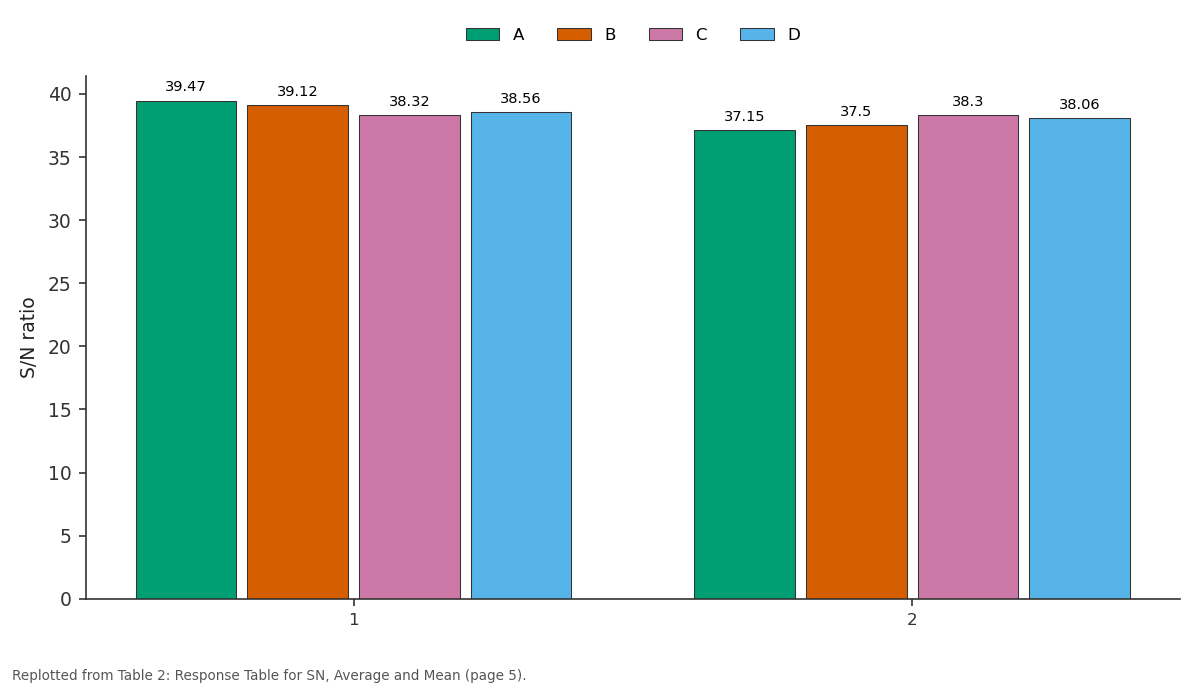
A and B and more: 1 vs 2
Replotted from Table 2 (page 5) of the original paper. Every bar is the paper's own table value.
View source evidence ↗Figures & tables
From the original paper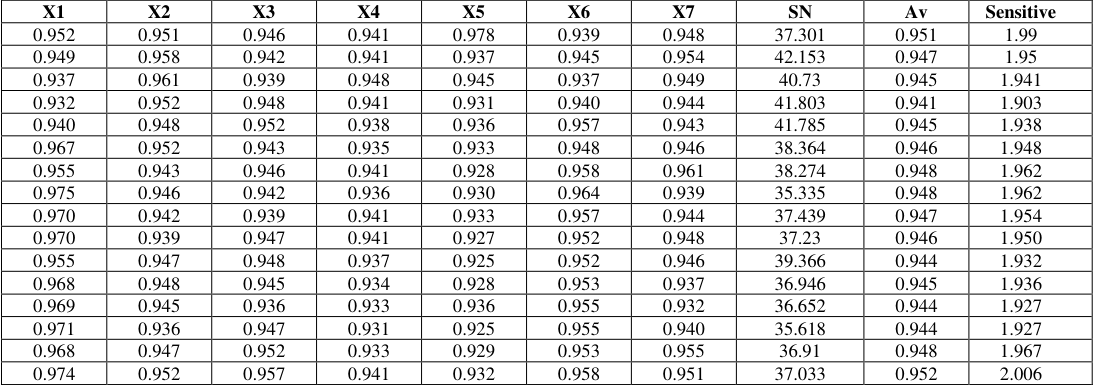 Table 1
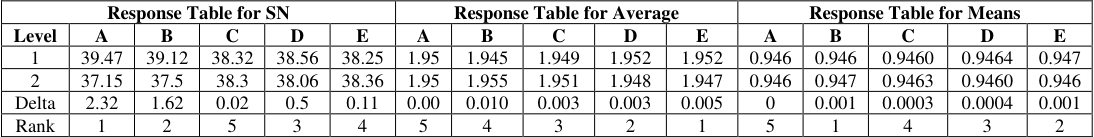 Table 2
 Table 3
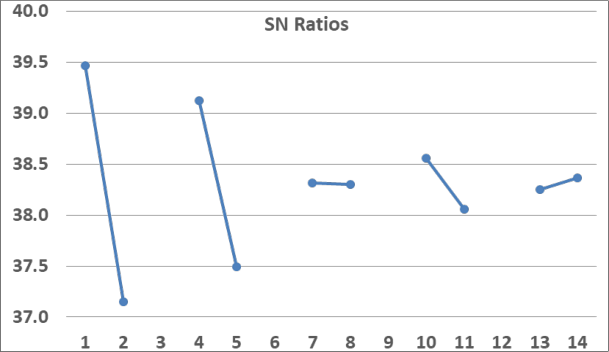 Figure 1
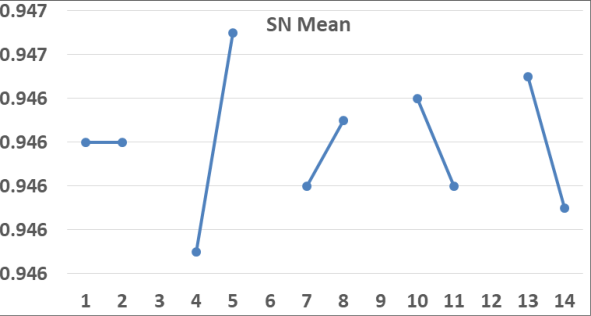 Figure 2
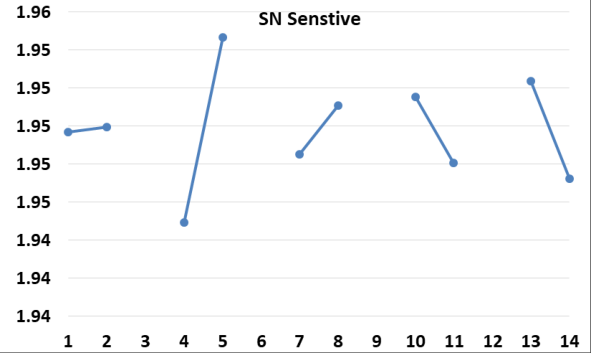 Figure 3
 Figure 3
Introduction
Statistical quality control methods are a collection of strategies and scientific techniques to study many different problems and have a large area of study. Statistical quality control came from Dr. Walter Shewhart in 1924 [6] . A crucial component of making sure a good or service fulfills the required standard of quality is quality control. It entails keeping an eye on and testing the good or service to find and fix any flaws or problems. Quality control is essential in ensuring customer satisfaction, reducing costs, and improving overall efficiency. Quality control using the S/N ratio is an integral part of the Taguchi method, a systematic approach to G.Taguchi developed the new method to optimize the design of manufacturing processes product. One of the key parameters used in quality control is the signal-to-noise (S/N) ratio, to evaluate the quality of a product or service by comparing the desired signal with the noise or unwanted variation in the output. The Taguchi method is a statistical technique that uses the S/N ratio to optimize product design and manufacturing processes. Modern industry aims to reduce costs while putting more of an emphasis on the steps an organization takes to ensure it is producing a high-quality good or service. Measurable characteristics and specifications must be created in order to compare the actual qualities of the good or service with them in order to apply quality control effectively. Since 1960, we have been using Taguchi methods to improve the quality starting with the specification and product planning [3,4] . The signal-to-noise ratio (SNR) and the noise-to-signal ratio (NSR), are two main types of S/N ratio. SNR measures of ratio of the power of the signal to the power of noise. Both SNR and NSR are significant metrics in many other domains and are used in quality control to assess a product's quality.
There are three different kinds of noise factors: between-product noise, inner noise, and external noise. The validity of several of Taguchi's techniques is debatable theoretically. One of them is his utilization of exterior arrays, which might be a component of the standard experimental layout. However, issues with experimental design are not our main concern. His advice on using signalto-noise (S/N) ratios to create robust designs is more pertinent. Good mean settings must be used in a robust design for the product to be resilient to variation. In other words, we are interested in both means and variances. However, according to Taguchi, data can be transformed using S/N ratios in such a way that both mean and variance can be optimized simultaneously [3,5,11] . The signal-to-noise (SN) ratio is then analyzed to identify the preferable parameter values, with the best factor levels that maximize the right SN ratio depending on the intended performance response, there 12 The signal-to-noise ratio serves as a gauge of a measuring system's quality. The quality increases with an increasing SN ratio. To evaluate measuring methods as well as the functionality of goods and processes, Taguchi expanded the SN ratio idea as employed in the communication sector [5] . Different types of standard SN ratios kinds of noise factors Smaller is better: In this case,the magnitude that we want to minimize in this instance is the squared response. Alternatively, the following transformation can be minimized to achieve this:
Nominal is best: Here, Taguchi looks at the statistic
Larger is better: In this case we may select l/x, as the response that we should minimize, leading to
To get the desired mean value, the main strategy is to choose settings that have a high signal-to-noise ratio, or a relatively strong signal, and then use other factors to adjust the mean.
The United States has been using a new quality engineering method known as the Taguchi method since the 1980s. This method is distinct from the quality engineering detailed method.
Taguchi's method is a robust design based on the following three procedures: 1. Orthogonal array.
2. SN ratio, 3. Loss function.
These three procedures are not robust design purses because they are used to evaluate technical means or products [6,7] .
Prior to designing robustness, we must comprehend what robustness means. When the true values of the signal factor levels are unknown, the variation of samples is used. After calculating the signal factor variation (SM) and subtracting it from the total variation (ST), the residual is regarded as the error term. As in the next two examples, the overall variation varies based on what is anticipated from the linear relationship.
Proportional equation ST =SM+ Se
Linear equation: ST =Sm+ SM + Se
These two cases a basic concept: Calculation of the effect, SM, of the signal factor, M, and the general mean, Sm, with different degrees of freedom. cannot calculate the total variation when the true value is known. The total effect (ST) and (SM), is obtained as follows:
Where k is the degrees of freedom of the signal variation (SM).
The error variation as equation:
Where the degrees of Freedom of the error is:
The error variance is becomes
The variance of signal factor is obtained as:
The S/N ratio is determined by:
𝑉 𝑒 (8) Because all production processes can produce different outputs for different products, the dynamic SN ratio is an important application to improve the robustness of the process product function to develop a group of products.
No Signal Factor (Non-dynamic SN Ratio) [2,3,4,8] The non-dynamic S/N ratio is a type of signal-to-noise ratio that considers the mean and standard deviation of a response variable. Usually, there are upper and lower limits to specifications. The type I case is one in which all of the data are positive. Data of type II is mix up of both positive and negative values. The first stage in two-step optimization for a nominal-the-best application is to minimize variability around the average by maximizing the SN ratio. The average must be adjusted to the target in the second step.
When the nominal-optimal S/N ratio is explained as follows SN = desired output undesired output
SN = deffect of the average variability around the average
In applications where nominal-the-best is used, the data is positive. This is particularly true if the output response is energyrelated, in which case there shouldn't be any negative data because zero input should result in zero output from the system. Here are the calculations for a nominal-the-best SN ratio.as follows.
𝑦 1 , 𝑦 2 , … , 𝑦 𝑛 (𝑓 = 𝑛)
The Average variation, SN is
The error variation, Se is
The error variance, Ve, is the error variation divided by its degrees of freedom:
The S/N ratio, denoted by Ƞ is given by:
The Sensitivity is given by:
When negative values are included in the experiment results, the positive and negative values cancel each other out, rendering the Sm calculation useless. As a result, it is impossible to gather data on average or sensitivity. In this instance, the S/N ratio computation reveals only variability. Compared to type I, it is less informative. From a conceptual standpo, the SN ratio gives the following information:
The S/N ratio is calculated as follows where there are n pieces of data: y1, y2,., yn. The error variation is:
And the S/N ratio is given by:
Two Types of S/N ratio 1-Smaller-the-Better, When minimizing the output value is the goal and there are no negative data, the smaller-the-better type is employed. The target value in this scenario is A smaller-the-better SN ratio is calculated as:
Larger-the-Better
When maximizing output is the goal, the larger-the-better approach is adopted as long as there are no negative data points. The target in this scenario is infinity.
It is advised to combine this kind of SN ratio with the smaller-is-better kind when creating an SN ratio for a non-dynamic operating window [9,10,12] . The larger-the-better SN ratio is given by:
The Gain and Optimum of S/N Ratios [1,5] The Gain is the optimum of S/N ratio calculate as this equation: The equation that follows to define the gain as well:
Variability Re duction=1-(0.5) Gain/ 6 …17
In order to predict the optimum condition, the expected mean at the optimal settings (Y) is calculated by using the following model.
YActual S/N = T -(A1-T) + (B1-T) + (C1-T) + (18) k = Number of variables R = The value of S/N ratio of level T = Total of SN
YActual S/N = T -(A1-T) + (B1-T) + (C1-T) + (18) k = Number of variables R = The value of S/N ratio of level T = Total of SN
Role of orthogonal arrays
The primary function of orthogonal as in robust engineering is to enable engineers to assess a product design in terms of cost and robustness against noise. An inspection tool called the OA is used to stop "poor designs" from moving "downstream. By reducing the number of experiments, the robust design's use of orthogonal arrays aims to estimate the effects of various factors and necessary interactions. and to determine variables that are useful while using the fewest possible variable combinations. The variables are allocated to the array's various array [1,5] .
Numerical Application
This paper used the current data of Lime Saturation Factors (L.S.F) of cement. The L.S.F value depends on five chemical elements such as (SiO2, Al2O3, Fe2O3,CaO, and SO3), where the value of L.S.F is an equation:
shown L.S. F= (CaO2-0.8*SO3)/(2.5*SiO3+2.5*Al2O3+0.5*Fe2O3).
The data are collected from chemical laborers with sample sizes (7*16) as shown in table (1).
To calculate the S/N ratio for the data using the Taguchi Orthogonal Array Design of 16 runs with 5 variables with two levels using L16(25). The corresponding S/N ratios, mean and the sensitivity of the SN ratio is calculated by equation (12) as shown in the table (1). Table (2) shows the response of S/N ratios, response of average and response of mean of data with two levels and calculating the delta and rank for two levels. And the first rank of SN is X1, for average is X5 and for mean is X2. 1)'s SN ratio, from level 1 the value (X1, X2, and, X4) has a higher SN ratio, which means that it has a relatively strong impact on variability, these variables are significant and useful. from Level 2-the value of (X5)has a higher SN ratio. It has a relatively weak impact on variability. Variables (X3) are harming discrimination, and are not significant. 2. In Fig ( 2)'s mean SN ratio, for the Level, the higher value of SN ratio is (X4, X5) indicating a relatively strong influence on variability. These are important and practical variables. the variable (X2, and X3) of Level 2 has a higher SN ratio. It barely affects variability at all. Variables (X1) are not significant but hurt discrimination. 3. Sensitive Fig ( 3), shows that the higher SN ratio of level 1 is (X4, X5), which it is means that it has a relatively strong impact on variability. These variables are important significant and useful.
The SN ratio is higher in Level 2 (X2, and X3). It has a relatively weak impact on variability. Variables (X1) are harming discrimination, and are not significant. From response table (2) of the S/N ratio used to determin the optimum S/N ratio, as YOpt S/N, denotes the minimum value from Level 1,2 for the (5) variables.
Where T is the total value. The original equation of YOpt, YActual, and variability reduction, as shown in table (3) where the YActual SN denotes the maximum value. The gain between current and optimal Gain = (Average S/N Ratio) Level 1 -(Average S/N Ratio) Level 2 where the variability reduction=1-(0.5) Gain/ 6
Conclusion
The results of this paper consider Taguchi's quality for calculating the SN ratio to the implication of a finite target ratio, to identify the useful set of origin variables simply. To show the higher level of SN ratio for (X1, X2, X3, X4, X5), which means that it has a relatively strong impact on variability.
Acknowledgement
To separate between which variables are significant and useful, and not useful. Determine the YOpt, YActual, variability reduction, and the gain between current and optimal. The value of optimized YOpt S/N and YActual SN for the original 5 variables in Level 1 and Level 2 are (36.034,236.029), and the value of gain is (0.009) with Variability Reduction is 0.101%.
Figures and tables from the paper
| X1 | X2 | X3 | X4 | X5 | X6 | X7 | SN | Av | Sensitive |
|---|---|---|---|---|---|---|---|---|---|
| 0.952 | 0.951 | 0.946 | 0.941 | 0.978 | 0.939 | 0.948 | 37.301 | 0.951 | 1.99 |
| 0.949 | 0.958 | 0.942 | 0.941 | 0.937 | 0.945 | 0.954 | 42.153 | 0.947 | 1.95 |
| 0.937 | 0.961 | 0.939 | 0.948 | 0.945 | 0.937 | 0.949 | 40.73 | 0.945 | 1.941 |
| 0.932 | 0.952 | 0.948 | 0.941 | 0.931 | 0.940 | 0.944 | 41.803 | 0.941 | 1.903 |
| 0.940 | 0.948 | 0.952 | 0.938 | 0.936 | 0.957 | 0.943 | 41.785 | 0.945 | 1.938 |
| 0.967 | 0.952 | 0.943 | 0.935 | 0.933 | 0.948 | 0.946 | 38.364 | 0.946 | 1.948 |
| 0.955 | 0.943 | 0.946 | 0.941 | 0.928 | 0.958 | 0.961 | 38.274 | 0.948 | 1.962 |
| 0.975 | 0.946 | 0.942 | 0.936 | 0.930 | 0.964 | 0.939 | 35.335 | 0.948 | 1.962 |
| 0.970 | 0.942 | 0.939 | 0.941 | 0.933 | 0.957 | 0.944 | 37.439 | 0.947 | 1.954 |
| 0.970 | 0.939 | 0.947 | 0.941 | 0.927 | 0.952 | 0.948 | 37.23 | 0.946 | 1.950 |
| 0.955 | 0.947 | 0.948 | 0.937 | 0.925 | 0.952 | 0.946 | 39.366 | 0.944 | 1.932 |
| 0.968 | 0.948 | 0.945 | 0.934 | 0.928 | 0.953 | 0.937 | 36.946 | 0.945 | 1.936 |
| 0.969 | 0.945 | 0.936 | 0.933 | 0.936 | 0.955 | 0.932 | 36.652 | 0.944 | 1.927 |
| 0.971 | 0.936 | 0.947 | 0.931 | 0.925 | 0.955 | 0.940 | 35.618 | 0.944 | 1.927 |
| 0.968 | 0.947 | 0.952 | 0.933 | 0.929 | 0.953 | 0.955 | 36.91 | 0.948 | 1.967 |
| 0.974 | 0.952 | 0.957 | 0.941 | 0.932 | 0.958 | 0.951 | 37.033 | 0.952 | 2.006 |
Table text extracted from the original PDF; superscript letters are shown inline. The original table image is below.
View original table image
| Response Table for SN | — | — | — | — | — | Response Table for Average | — | — | — | — | Response Table for Means | — | — | — | — |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Level | A | B | C | D | E | A | B | C | D | E | A | B | C | D | E |
| 1 | 39.47 | 39.12 | 38.32 | 38.56 | 38.25 | 1.95 | 1.945 | 1.949 | 1.952 | 1.952 | 0.946 | 0.946 | 0.9460 | 0.9464 | 0.947 |
| 2 | 37.15 | 37.5 | 38.3 | 38.06 | 38.36 | 1.95 | 1.955 | 1.951 | 1.948 | 1.947 | 0.946 | 0.947 | 0.9463 | 0.9460 | 0.946 |
| Delta | 2.32 | 1.62 | 0.02 | 0.5 | 0.11 | 0.00 | 0.010 | 0.003 | 0.003 | 0.005 | 0 | 0.001 | 0.0003 | 0.0004 | 0.001 |
| Rank | 1 | 2 | 5 | 3 | 4 | 5 | 4 | 3 | 2 | 1 | 5 | 1 | 4 | 3 | 2 |
Table text extracted from the original PDF; superscript letters are shown inline. The original table image is below.
View original table image
References
6 in the original paper- Ahilan C, Kumanan S, Sivakumaran N. Application of grey based taguchi method in multi-response optimization of turning process, Advances in Production Engineering & Management. 2010;5(3):171-180. ISSN 1854-6250
- Taguchi G, Jugulum R. The Mahalanobis-Taguchi Strategy Copyright © 2002 John Wiley & Sons, Inc; c2002.
- Kawa M, Rashid J. Comparative between the MEWMA and Mahalanobis Distance Control Chart, Kurdistan Journal of Applied Research -KJAR. 2021;6(2):94-104.
- Yusoff N, Ramasamy M, Yusup S. Taguchi's parametric design approach for the selection of optimization variables in a refrigerated gas plant, 2010 Published by Elsevier B.V. on behalf of The Institution of Chemical Engineers; c2010.
- Teruo Mori, PhD, PE translated by Shih-Chung Tsai, PhD, CQE, Taguchi Methods Benefits, Impacts, Mathematics, Statistics, and Applications, 2011, ASME, 3 Park Avenue, New York, NY 10016, USA; c2011.
- Roy R. A Primer on the Taguchi Method, Copy right 1990 by Catalog Card Number 89-14736; c1990.
Cited by 42
From OpenAlex, OpenCitations and reference lists read by Scinovex
- Robustness in deep learning models for medical diagnostics: security and adversarial challenges towards robust AI applications ↗
Haseeb Javed, Shaker El–Sappagh, Tamer Abuhmed · Artificial Intelligence Review · 2024
The current study investigates the robustness of deep learning models for accurate medical diagnosis systems with a specific focus on their ability to maintain performance in the presence of adversarial or noisy inputs. We examine factors that may influence model reliability, including model complexity, training data quality, and hyperparameters; we also examine security concerns related to adversarial attacks that aim…
❝ 182PDF - Effect of Drilling Parameters on Surface Roughness and Delamination of Ramie–Bamboo-Reinforced Natural Hybrid Composites ↗
Krishna Kumar P, Gaddam Lokeshwar, Chamakura Uday Kiran Reddy, Arun Jyotis, Surendra Shetty, Subash Acharya et al. · Journal of Manufacturing and Materials Processing · 2024
Plastics reinforced with glass fiber have a significant likelihood of being replaced by natural fiber hybrid composites (NFHCs). Making holes helps in part assembly, which is a crucial activity in the machining of composite constructions. As a result, choosing the right drill bit and cutting parameters is crucial to creating a precise and high-quality hole in composite materials. The present…
❝ 13PDF - Optimizing Solar Drying Chamber Performance: Taguchi Analysis of Uniformity Enhancement Methods ↗
Halefom Kidane, István Farkas, János Buzas · International Journal of Energy Research · 2025
Solar drying is an ancient yet sustainable method for preserving agricultural products. However, a key challenge in this process is achieving uniform airflow distribution, as uneven airflow can result in inconsistent drying and reduced product quality. To address this issue, the study incorporates flow enhancement tools such as baffles and swirlers to the plenum of the drying chamber. The result…
❝ 8PDF - Analysis and optimization of FDM printing process of PETG parts using statistical and machine learning methods ↗
Anamul Hasan, Synthia Ferdouse, Mohammad Tafsir Ahmed Shiddiki, Zhong Hu · Progress in Additive Manufacturing · 2026
❝ 6 - Design, fabrication, and optimization of a portable plug-and-play biogas filtration unit for small-scale biogas plants using the Taguchi method ↗
Nainil Patel, Vandan Shah, Parth P. Prajapati · Biomass and Bioenergy · 2025
❝ 5 - Optimization of arc quenching parameters for enhancing surface hardness and line width in S45C steel using Taguchi method ↗
Van–Thuc Nguyen, Pham Son Minh, Hung-Son Dang, Nguyen Ho · PLoS ONE · 2024
This study investigates the impact of arc length, current intensity, travel speed, and gas flow rate on surface hardness and line width during arc quenching process of S45C steel. The current intensity has the greatest influence on the surface hardness of S45C steel, followed by the travel speed, gas flow rate, and arc length. Using the Taguchi method, the optimal…
❝ 5PDF - Novel protocol for isolation and transient transformation of Rhodes grass (Chloris gayana) protoplasts ↗
Kellie Maybery-Reupert, Khageswor Giri, Matthew Hayden, Noel O. I. Cogan, Daniel A. Isenegger · In Vitro Cellular & Developmental Biology - Plant · 2025
Abstract Rhodes grass (Chloris gayana) is a warm-season C4 grass currently grown as a forage in some tropical regions, with anticipated future application in areas affected by climate change. However, there are few resources available for this grass, with few genomic resources and only one established transformation system, thus limiting the application of biotechnology methods for its improvement. Protoplast transformation…
❝ 4PDF - Hydrodistillation, comparative analysis and optimization of essential oils from Thymus schimperi R, Thymus serrulatus R, and Ocimum lamiifolium Hochst ex Benth ↗
Sisay Belachew Mebrate, Adane Flatie Alemu, Aychew Mekuriaw Tegegne, Minbale Gashu, Gebremariam Ketema · Scientific Reports · 2026
Essential oils are valuable natural products that are currently popular worldwide due to their positive effects on human health and their significant role in preventing and curing diseases. The increasing prevalence of antibiotic-resistant pathogens poses a major global health challenge, limiting the effectiveness of conventional antimicrobial therapies. Medicinal plants such as Thymus schimperi R., Thymus serrulatus R., and Ocimum lamiifolium…
❝ 3PDF - On Design and Development of PLA Composite-Based 3D-Printed Sensor-Embedded Cerclage Strip for Tensile Loading Applications ↗
Gurwinder Singh, Rupinder Singh, Amrinder Pal Singh, Minhaz Husain, Vinay Kumar · Journal of Materials Engineering and Performance · 2025
❝ 3 - Investigating Sodium Percarbonate for Upgrading Torrefied Spent Coffee Grounds as Alternative Solid Biofuel by Taguchi Optimization ↗
Wei-Hsin Chen, Kuan-Ting Lee, Ji-Nien Sung, Ning Hu, Yun-Sen Xu · Energies · 2025
Producing solid biofuels with high calorific value and high storage stability under limited energy consumption has become a crucial focus in the global energy field. Low temperature torrefaction below 300 °C is a common method for producing solid biofuels. However, this approach limits the carbon content and higher heating value (HHV) of the resulting biochar. Sodium percarbonate is a solid…
❝ 3PDF - Hybrid Taguchi and Machine Learning Framework for Optimizing and Predicting Mechanical Properties of Polyurethane/Nanodiamond Nanocomposites ↗
Markapudi Bhanu Prasad, Borhen Louhichi, Santosh Kumar Sahu · Computer Modeling in Engineering & Sciences · 2025
This study investigates the mechanical behavior of polyurethane (PU) nanocomposites reinforced with nanodiamonds (NDs) and proposes an integrated optimization–prediction framework that combines the Taguchi method with machi... | Find, read and cite all the research you need on Tech Science Press
❝ 3PDF - A non-conventional biodiesel process route from waste palm fatty acid distillate and ethyl acetate via esterification ↗
Akintomiwa Olumide Esan, Blessing Ayomide Olafimihan, Ibidotun Theophilus Olawoore, Mustapha Omenesa Idris, Nur Mazlini Razali, Tan Ee Sann · Scientific Reports · 2026
The high cost and food competition associated with conventional biodiesel feedstocks limit its widespread adoption. This research investigates using palm fatty acid distillate (PFAD), a low-cost industrial by-product which is high in free fatty acids (FFAs), as a sustainable feedstock. A novel glycerol-free esterification route was developed employing ethyl acetate as acyl acceptor and sulfuric acid as catalyst, producing fatty…
❝ 2PDF - Optimization of culture medium for probiotic bacterium Lacticaseibacillus casei UT1 to enhance biomass production using the Taguchi statistical method ↗
Saman Afshar, Gholamreza Zarrini, Nader Farsad-Akhtar · Journal of Microbiological Methods · 2025
❝ 2 - Multi objective optimization of cutting parameters of end milling operation by Taguchi Grey ↗
Shilpa Bhimrao Sahare, Prashant Dnyaneshwar Kamble, Jayant P Giri, Neeraj Sunheriya, T. Sathish, Rajkumar Chadge et al. · Interactions · 2024
❝ 2 - Maximising CO2 sequestration via simultaneous milling and carbonation of steel slag: A Taguchi-driven optimisation approach ↗
Nina Miladinović, Luka Ceyssens, Giuseppe Granata, Tom Van Gerven · Process Safety and Environmental Protection · 2026
Steel slags, byproducts of the steelmaking industry, pose a significant environmental burden due to their large volume and limited reuse opportunities. CO 2 sequestration represents a promising utilisation route, enabled by their diverse mineral composition. However, conventional carbonation methods are often slow and require rigorous conditions. This study presents a rapid and intensified approach for carbon capture via simultaneous milling…
❝ 1PDF - Adaptive Stochastic Approach for Evaluating Service Level Using a (SIM-ESL) Module Developed for Optimizing Product Availability and Order Accuracy ↗
Samah A. Aufy, R Abduladheem Jabbar, Waad Q. Shiaa · Management Systems in Production Engineering · 2025
Abstract Inventory decisions are both high risk and high benefit throughout supply chain. Inventory management plays a crucial role since it assists manufacturing firms enhance their efficiency and competitiveness. Service level is a basic performance indicator of shortage inventory when an order is placed. Precise forecasts and optimum level of inventory can decrease the stock-outs and enhance the inventory service…
❝ 1PDF - Management-Oriented Assessment of Transport Service Quality Using Logistics Monitoring System and Harrington’s Desirability Function in Support of SDG 9 ↗
Віктор Аулін, Оleg Lyashuk, Dmytro Mironov, Piotr Staliński, Marek Rutkowski, Sergiy Lysenko · Sustainability · 2025
The quality of transport services is not only a measure of operational efficiency but also an important factor of strategic logistics management in the pursuit of sustainable development. This study identifies five key transport service quality indicators (timeliness, routing, economy, safety, efficiency) and uses data from a logistics monitoring system to assess them with Harrington’s desirability function. Each indicator’s performance…
❝ 1PDF - Taguchi-based parameter optimization of ultrasonic vibration–assisted scribing for silicon wafer singulation ↗
Ming Cheng Tsai, Muslim Hussain Rather, Jenq Shyong Chen · The International Journal of Advanced Manufacturing Technology · 2025
❝ 1 - Optimization of Fused Deposition Modeling (FDM) Process for Small-Scale PEEK Medical Devices ↗
AmirDanial Azimi, Leila Jannesari Ladani, Jafar Razmi, David G. Lott, Brent A. Chang · Journal of Manufacturing and Materials Processing · 2025
Additive manufacturing (AM) of polyetheretherketone (PEEK) offers a promising route for producing lightweight, biocompatible, and patient-specific medical implants with complex geometries. This study investigates and optimizes fused deposition modeling (FDM) parameters for fabricating small-scale PEEK medical components with improved dimensional accuracy and surface quality. PEEK’s high processing temperature and thermal contraction make precision printing of fine features challenging. A Taguchi…
❝ 1PDF - Intelligent Workforce Scheduling in Manufacturing: An Integrated Optimization Framework Using Genetic Algorithm, Monte Carlo Simulation, and Taguchi Method ↗
Berrin Denizhan, Elif Yıldırım, Beyza Fındıklı, Mehmet Efe Erbaş, Batuhan Öz, Bengisu Derya · Systems · 2025
Small and medium-sized enterprises (SMEs) constitute a substantial share of industrial production. However, their operational performance is frequently constrained by delivery delays caused by inefficiencies in workforce scheduling and task sequencing. These limitations reduce overall competitiveness, particularly in project-based manufacturing environments where task heterogeneity and multi-skill variability are prominent. To address this challenge, this study develops an artificial intelligence based…
❝ 1PDF